Glass vs. PET Carbonated Beverage Filling Lines: Configuration, Suitability, and Technical Trade-offs
Glass vs. PET Carbonated Beverage Filling Lines: Configuration, Suitability, and Technical Trade-offs
For procurement managers and operations leads planning a new carbonated beverage facility, the choice between glass and PET (Polyethylene Terephthalate) bottles is the single most influential decision on production line architecture. Unlike non-carbonated water filling—where Chuxin Mingwei specializes in atmospheric pressure systems—carbonated beverage production introduces complex variables: internal pressure management, gas retention, and distinct sterilization pathways.
This comparison breaks down the configuration differences, application suitability, and critical technical parameters you must define before engaging an equipment manufacturer.
1. Core Configuration Differences: Handling and Conveyance
The physical properties of the container dictate the upstream and downstream mechanics of the filling line.
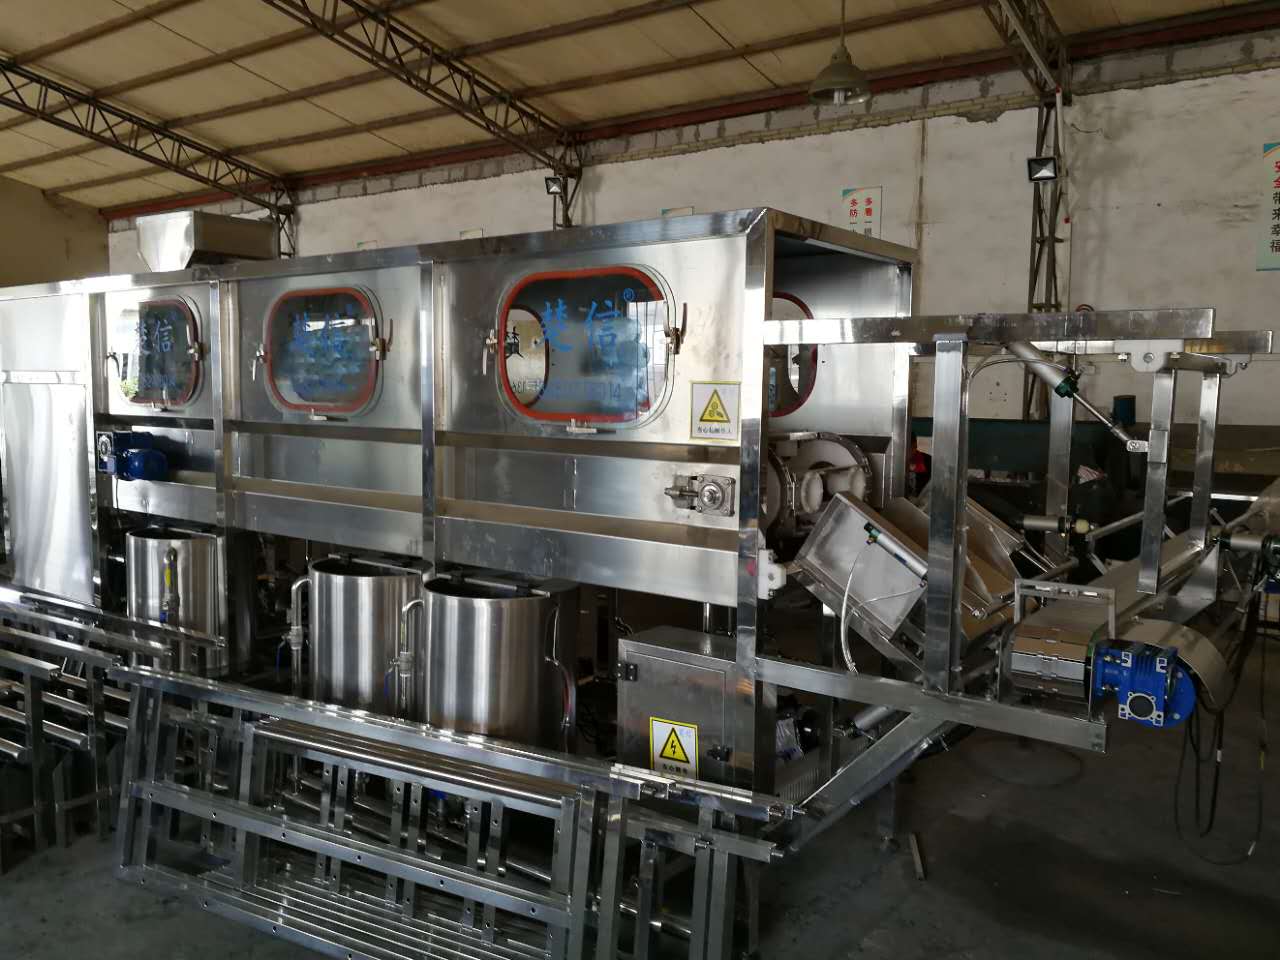
Glass Bottle Lines
- Conveyance System:*
- Requires heavy-duty chain conveyors with lubrication systems to manage high friction and weight. Glass bottles are rigid but brittle, necessitating gentle transfer stars and guides to prevent breakage.
- Cleaning Process:*
- Typically employs air-rinsing or vacuum suction to remove dust. Because glass can withstand high temperatures, some configurations allow for hot water rinsing, though this increases energy load.
- Integration:*
- Usually operates as a standalone filling unit. Bottle supply is external (purchased pre-formed), requiring significant storage space for empty crates or pallets.
PET Bottle Lines
- Conveyance System:*
- Uses lightweight neck-handling conveyors. Since PET bottles are prone to tipping when empty, modern lines often integrate Blow-Fill-Cap technology, where bottles are blown immediately before filling, eliminating the need to store and convey empty containers.
- Cleaning Process:*
- Relies heavily on sterile air rinsing or chemical sterilants (like peracetic acid) followed by sterile water rinses. PET cannot withstand high heat during the filling process.
- Integration:*
- High potential for compact layouts if integrating a blow-molding machine directly upstream, reducing footprint and contamination risk.
2. The Filling Technology: Isobaric Pressure Control
Regardless of the bottle material, carbonated beverages require isobaric filling (counter-pressure filling). The liquid must be filled under the same pressure as the CO2 saturation inside the tank to prevent foaming and gas loss.
- Glass Compatibility:*
- Glass's rigidity makes it inherently suitable for high-pressure filling. The filling valve seals against the rigid mouth of the bottle, allowing for precise pressure equalization. Glass lines can also accommodate hot filling (up to 85-90°C) for certain preservative-free products, followed by tunnel pasteurization, as the container will not deform.
- PET Constraints:*
- PET is sensitive to temperature and pressure stress.
- Temperature Limit:*
- Standard PET bottles generally cannot handle filling temperatures above 60-65°C without special heat-set treatment. Most carbonated PET lines operate as cold-fill systems.
- Pressure Management:*
- The filling valve must gently ramp up pressure to avoid bursting the preform or causing "petaling" at the base. The capping mechanism must apply torque carefully to ensure the plastic thread does not strip while maintaining a gas-tight seal.
3. Application Scope and Strategic Suitability
| Feature | Glass Bottle Line | PET Bottle Line |
|---|---|---|
| Primary Market | Premium beers, craft sodas, high-end mineral waters, returnable logistics. | Mass-market soft drinks, sparkling waters, ready-to-drink teas, export markets. |
| Production Speed | Moderate (limited by weight and breakage risk). | High (lightweight, integrated blowing allows >20,000 bottles/hour in large setups). |
| Sterilization | Tunnel pasteurization (post-fill) possible; robust against heat. | Aseptic cold-fill required; relies on sterile environment and chemical sterilization. |
| Logistics Cost | High (heavy weight, breakage risk, returnable crate management). | Low (lightweight, non-returnable, efficient shipping). |
| CAPEX Focus | Heavy machinery, crate washers, pasteurizers. | Blow-molding integration, sterile room construction, precise valve tech. |
4. Critical Technical Agreement Points
When specifying a carbonated filling line, vague requirements lead to operational failures. Procurement teams must clarify the following with the engineering team:
- CO2 Content Range: Define the exact volumes of CO2 (e.g., 2.5 to 4.5 volumes). Higher carbonation requires more sophisticated pressure relief valves and slower filling speeds to prevent foaming.
- Bottle Geometry Tolerance:
- For Glass: Specify neck finish standards and maximum allowable deviation in height/diameter.
- For PET: Define the preform weight and bottle wall thickness distribution. Thin-walled lightweight bottles require specialized low-torque capping heads.
- Temperature Constraints: Explicitly state the maximum filling temperature. If the product requires hot filling for shelf stability, confirm the PET bottle supplier provides heat-set containers, or opt for glass.
- Changeover Requirements: If running multiple SKUs, define the acceptable changeover time. Glass lines often require manual star-wheel changes; advanced PET lines may feature quick-change parts.
5. Implementation Boundaries and Risks
- Misapplication of Water Lines:*
- Standard purified water filling lines (like those Chuxin Mingwei supplies for still water) operate at atmospheric pressure. They cannot be simply upgraded to fill carbonated drinks without replacing the entire filling block, valve system, and pressure control logic.
- Facility Constraints:*
- Glass lines require reinforced flooring due to weight and space for crate washing/return loops. PET lines require strict cleanroom controls (ISO Class 8 or better) if operating in an aseptic cold-fill mode, as there is no post-fill pasteurization step.
- Maintenance Complexity:*
- Isobaric valves are more complex than gravity fillers. They require regular calibration of pressure sensors and sealing gaskets. Lack of trained operators is a common cause of CO2 loss and inconsistent fill levels.
Conclusion
Selecting between glass and PET for carbonated beverages involves balancing brand positioning against operational complexity. Glass offers premium appeal and thermal processing flexibility but incurs higher logistical and mechanical handling costs. PET offers speed and efficiency but demands rigorous temperature control and sterile processing environments.
For clients considering an expansion from still water to sparkling or flavored beverages, it is crucial to recognize that this is not a minor upgrade but a distinct project requiring specialized isobaric engineering.
Next Steps:
If your project involves carbonated products, do not rely on standard water line specifications. Contact our engineering team to discuss your specific CO2 levels, bottle dimensions, and thermal processing needs. We can help validate whether your current facility layout supports the heavy infrastructure of glass or the sterile zones required for PET.
Discuss Your Carbonated Project Requirements
Recommended
Bottled Spring Water Filling Production Line
Chuxin Mingwei’s customized bottled spring water filling production line is specifically...
Fully Automatic Bottled Purified Water Filling Production Line
Chuxin Mingwei’s customized fully automatic bottled purified water filling production li...
Clean Air Purification Systems
Custom-engineered air purification systems for water bottling and barrelled water fillin...