Operational Risk Boundaries for Automatic Barrel-Wrap Packaging at Maximum Speed
Operational Risk Boundaries for Automatic Barrel-Wrap Packaging at Maximum Speed
The Scenario: Pushing Capacity vs. Maintaining Integrity
For operations leaders in the beverage, food, and pharmaceutical sectors, the pressure to maximize output is constant. When deploying an automatic barrel-wrap packaging machine (often integrated into a full barrelled water filling line), the immediate instinct is often to increase the conveyor speed or wrap cycle rate to match the upstream filling capacity.
However, operating wrapping equipment at its theoretical maximum speed without adjusting downstream parameters creates a distinct set of operational risks. Unlike the filling process, where flow rates are controlled by valves and sensors, the wrapping process relies on mechanical tension, film viscosity, and thermal sealing consistency. Pushing these variables beyond their stable range can lead to film tearing, unstable pallets, and compromised hygiene barriers.
This article outlines the risk boundaries for high-speed barrel wrapping, focusing on the intersection of equipment capability, material behavior, and safety compliance.
Key Operational Risks at Maximum Speed
When running an automatic wrapping system at peak velocity, three primary failure modes emerge that directly impact product quality and site safety:
1. Film Tension and Seal Integrity Failure
At higher speeds, the time available for the heat seal bar to engage the film decreases. If the machine runs too fast, the seal may not reach the required temperature or dwell time, leading to weak bonds. Conversely, if the film feed tension is not synchronized perfectly with the conveyor speed, the film can stretch excessively or tear.
- Risk Indicator:*
- Visible wrinkles in the film, loose corners on the pallet, or seals that separate under light manual stress.
- Consequence:*
- A compromised barrier allows dust, moisture, or contaminants to enter the packaging during storage or transport, violating hygiene standards required for bottled spring water or purified water products.
2. Mechanical Instability and Pallet Toppling
Automatic wrapping machines rely on precise rotation speeds relative to the vertical lift mechanism. At maximum speed, centrifugal forces increase. If the load (e.g., 18.9L barrels) is not centered or if the film layer count is insufficient for the weight distribution, the pallet may become unstable during the spin cycle.
- Risk Indicator:*
- Excessive vibration in the machine frame, audible grinding noises from the turntable motor, or slight tilting of the load during rotation.
- Consequence:*
- In severe cases, this leads to load collapse, damaging the product (cracked barrels) and creating a significant safety hazard for nearby operators.
3. Sensor and Control System Latency
Modern systems use PLC-based controls to detect film breaks or misalignment. At maximum speed, the reaction time of optical sensors and photo-eyes becomes critical. If the film tears or the pallet shifts slightly off-center, the system must react within milliseconds to stop the cycle.
- Risk Indicator:*
- Frequent false alarms, delayed emergency stops, or the machine failing to detect a film break until after several layers have been applied incorrectly.
- Consequence:*
- Wasted film, inconsistent packaging quality, and potential damage to the machine's servo motors due to sudden stops.
Defining Acceptance Criteria and Boundaries
To optimize operations without crossing into unsafe territory, procurement managers and operations leads must establish clear acceptance criteria before ramping up speed. These boundaries should be defined in the technical agreement and verified during commissioning.
Material Compatibility Boundary
The wrapping machine is only as fast as the film it uses. Standard industrial stretch films have a specific elongation limit.
- Rule:*
- Do not exceed the manufacturer's recommended speed for the specific film gauge (microns) being used. If higher speeds are required, the film specification must be upgraded (e.g., higher tensile strength or pre-stretch ratio).
- Verification:*
- Run a test batch at the target speed and inspect the first 50 pallets for seal integrity and film tension uniformity.
Process Integration Boundary
Wrapping speed cannot be optimized in isolation. It must be balanced with the upstream barrel filling line and downstream clean air systems.
- Rule:*
- The wrapping station should not create a bottleneck that causes barrels to queue up against the machine inlet, nor should it run so fast that it outpaces the cooling or curing time required for any adhesive labels or shrink bands applied earlier.
- Verification:*
- Ensure the buffer zone between the filling line and the wrapper has sufficient capacity to absorb minor speed fluctuations without causing jams.
Safety and Compliance Boundary
All automated packaging equipment must adhere to local safety regulations regarding moving parts and emergency stops.
- Rule:*
- Safety guards and light curtains must remain functional regardless of speed. Emergency stop buttons must halt the machine within the specified distance (typically <0.5 seconds) even at maximum RPM.
- Verification:*
- Conduct regular safety audits to ensure that speed increases have not bypassed or altered safety interlocks.
Optimization Strategy: From Speed to Stability
Rather than simply turning a dial to "Maximum," a more effective approach involves optimizing the entire workflow:
- Calibrate Pre-Stretch Ratio: Adjust the pre-stretch rollers to ensure the film is stretched optimally before application. This reduces the force required to hold the load together, allowing for smoother operation at higher speeds.
- Synchronize PLC Logic: Work with the engineering team to fine-tune the PLC logic for acceleration and deceleration curves. Smooth transitions reduce mechanical shock compared to abrupt starts and stops.
- Monitor Real-Time Diagnostics: Utilize the HMI (Human-Machine Interface) to monitor torque loads and film tension in real-time. Set alerts for deviations rather than relying solely on visual inspection.
- Validate with Load Testing: Before full-scale deployment, run the machine with full-load pallets (e.g., 18.9L barrels) to verify stability. Empty pallet tests do not accurately reflect the dynamics of a fully loaded unit.
Conclusion
Operating an automatic barrel-wrap packaging machine at maximum speed offers potential throughput gains but introduces significant risks to film integrity, load stability, and operator safety. The optimal performance point is rarely the absolute maximum speed; it is the highest speed at which the system maintains consistent seal quality, structural stability, and safety compliance.
By defining clear boundaries for material compatibility, process integration, and safety protocols, operations teams can achieve sustainable efficiency without compromising product quality. For complex applications involving mixed barrel sizes or varying environmental conditions, a site-specific engineering review is essential to determine the true operational limits.
Next Steps
If you are evaluating the integration of automatic wrapping solutions into your beverage or industrial water production line, or if you need assistance optimizing existing equipment for higher reliability, our engineering team can provide a detailed assessment.
Contact Chuxin Mingwei today to discuss your specific capacity requirements, film specifications, and facility constraints. We specialize in delivering end-to-end engineering services that prioritize long-term stability and maintainability.
[Contact Our Engineering Team for a Site Assessment]
Recommended
Bottled Spring Water Filling Production Line
Chuxin Mingwei’s customized bottled spring water filling production line is specifically...
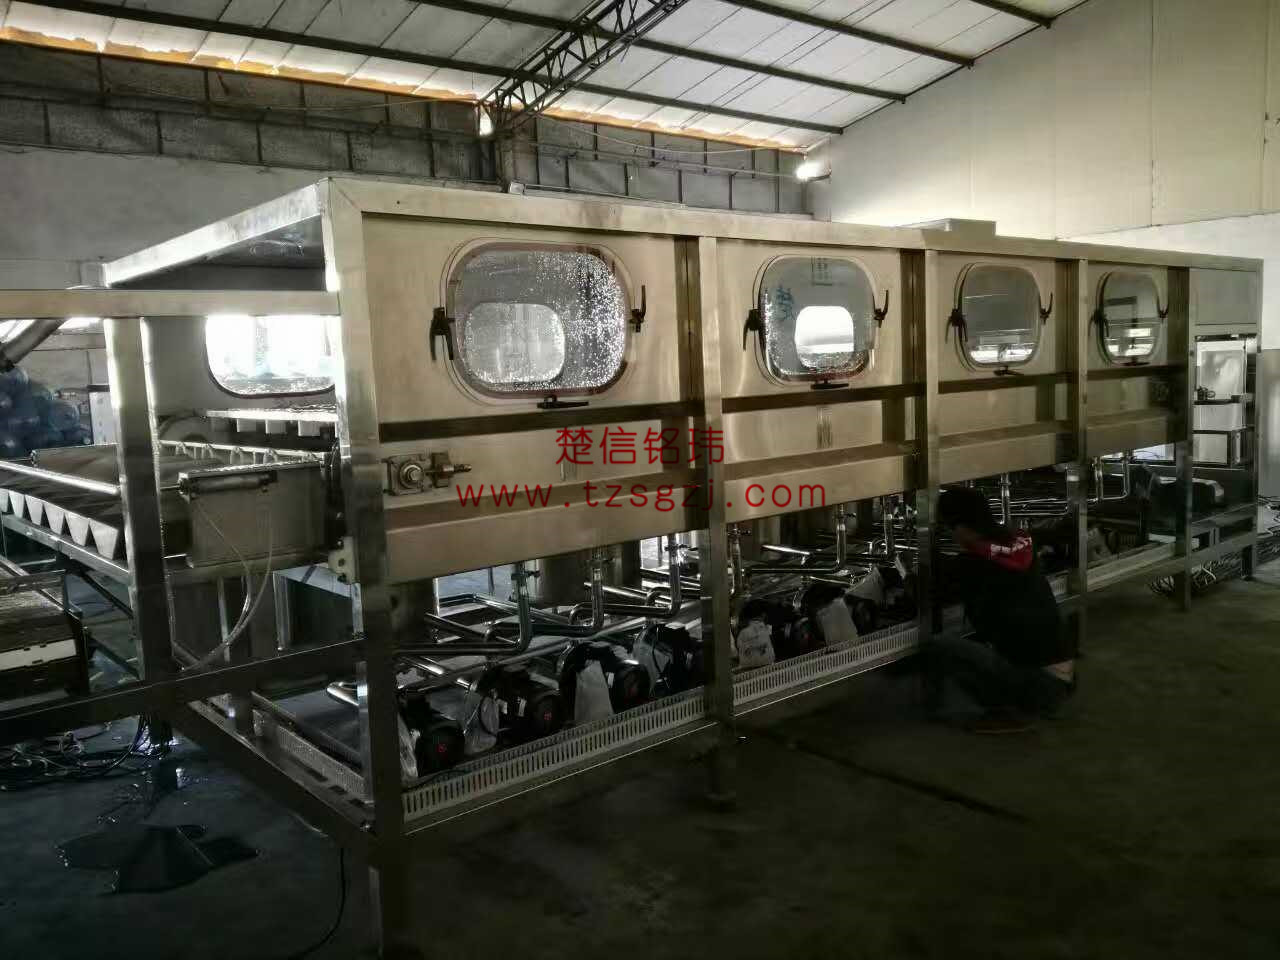
Fully Automatic Bottled Purified Water Filling Production Line
Chuxin Mingwei’s customized fully automatic bottled purified water filling production li...
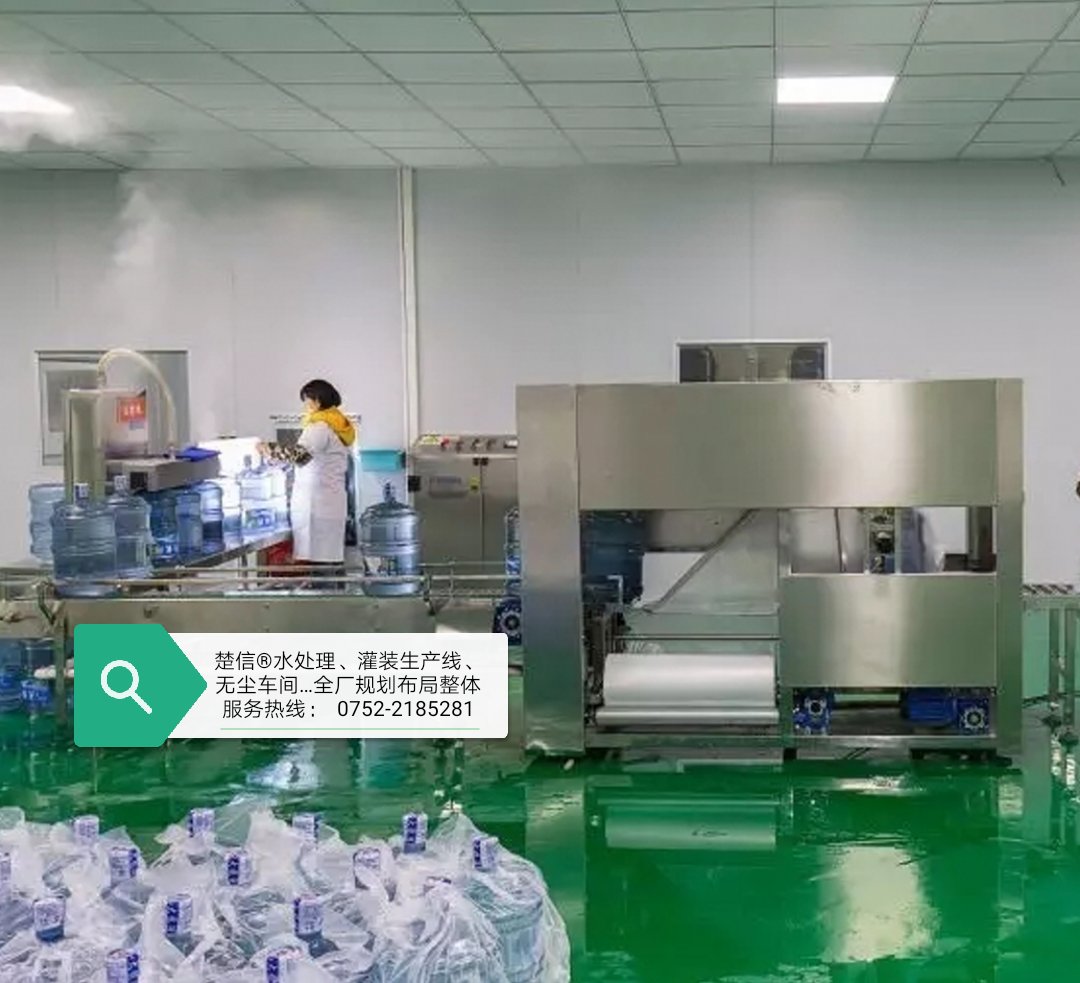
Clean Air Purification Systems
Custom-engineered air purification systems for water bottling and barrelled water fillin...